A food processing plant in Brampton needed a new floor for its boiler room, approximately 2,000 sq ft of plant space with boilers, pumps, water treatment equipment and overhead piping. The client asked that its name not be published. Request a free estimate to discuss your facility.
The Challenge
Boiler rooms are working spaces. The floor sees water around pumps and valves, maintenance traffic and equipment that cannot be moved. The new floor had to be installed around fixed boilers, pump skids, tanks and pipe supports, provide grip for maintenance staff and stay easy to clean.
The System
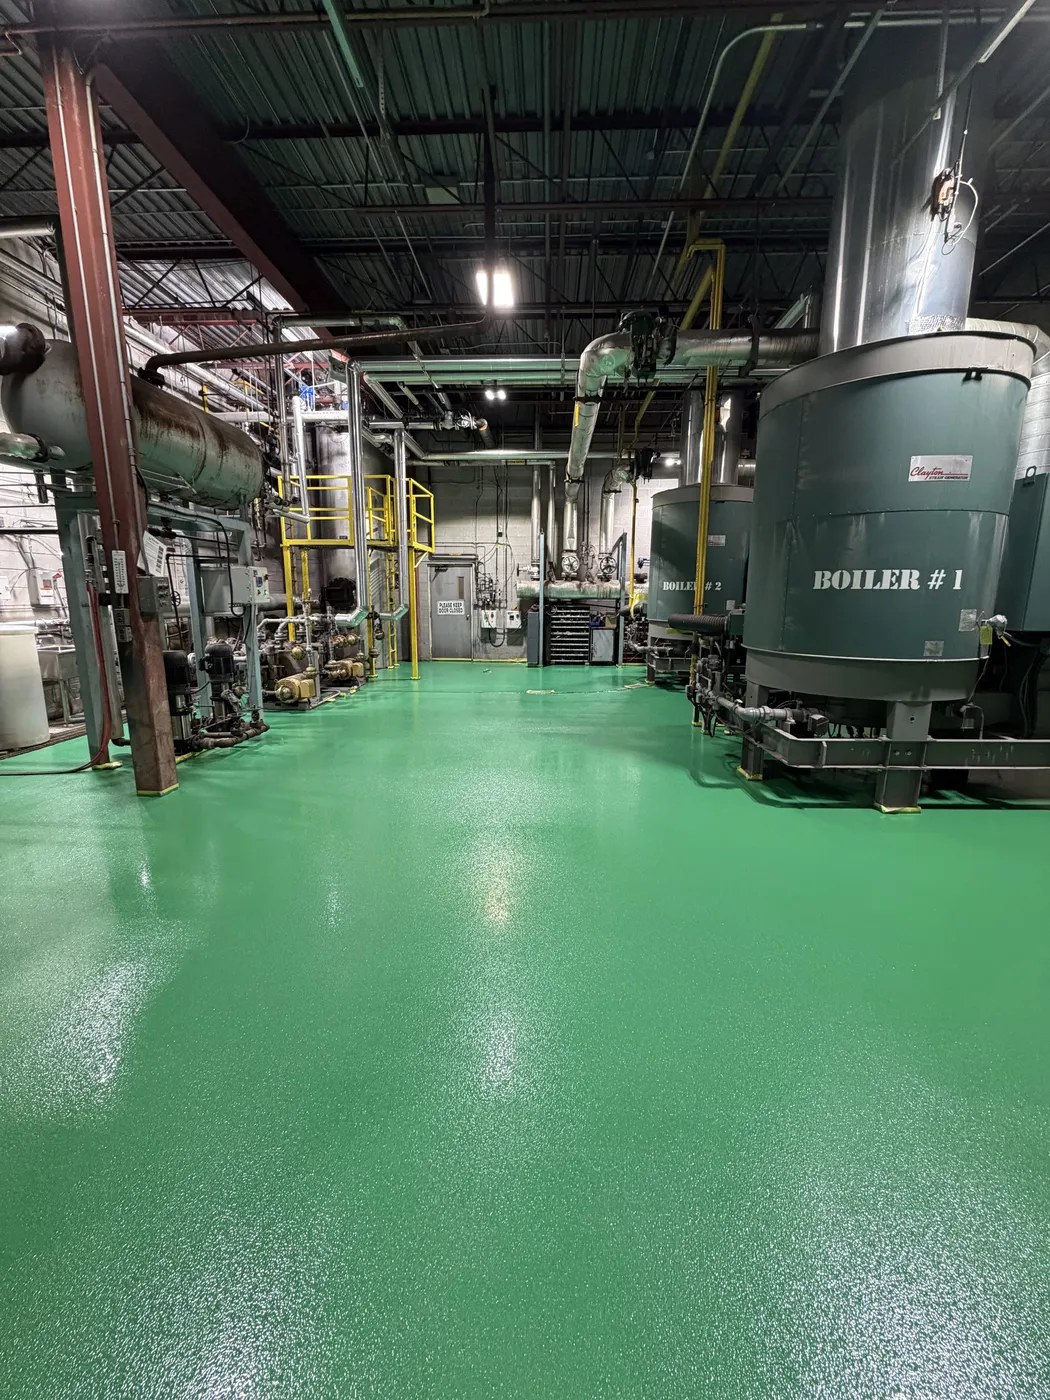
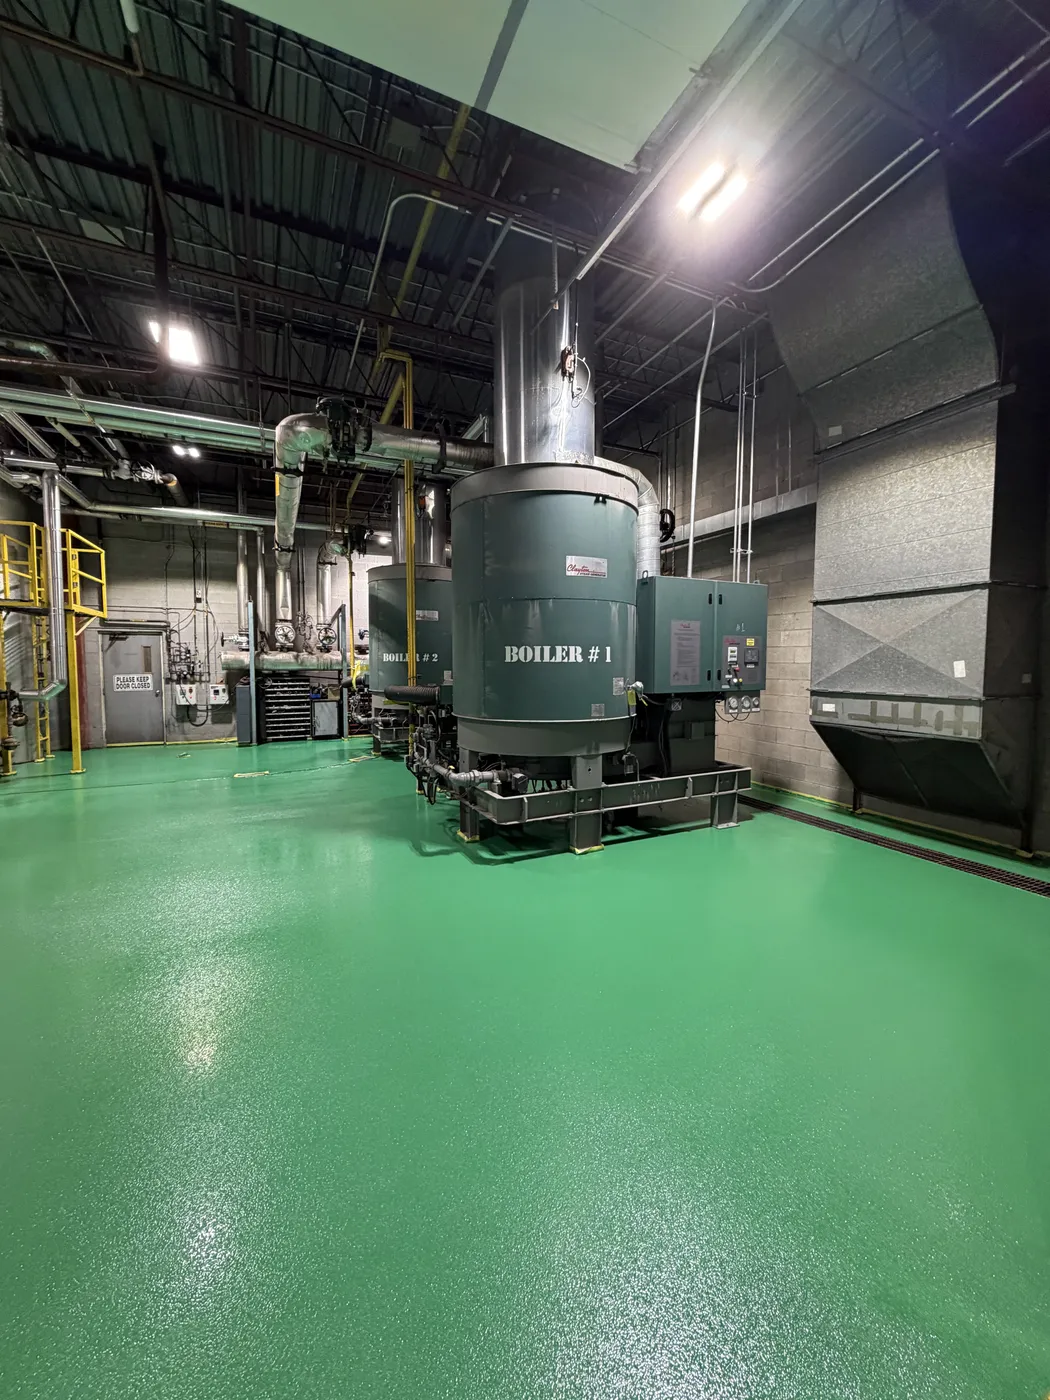
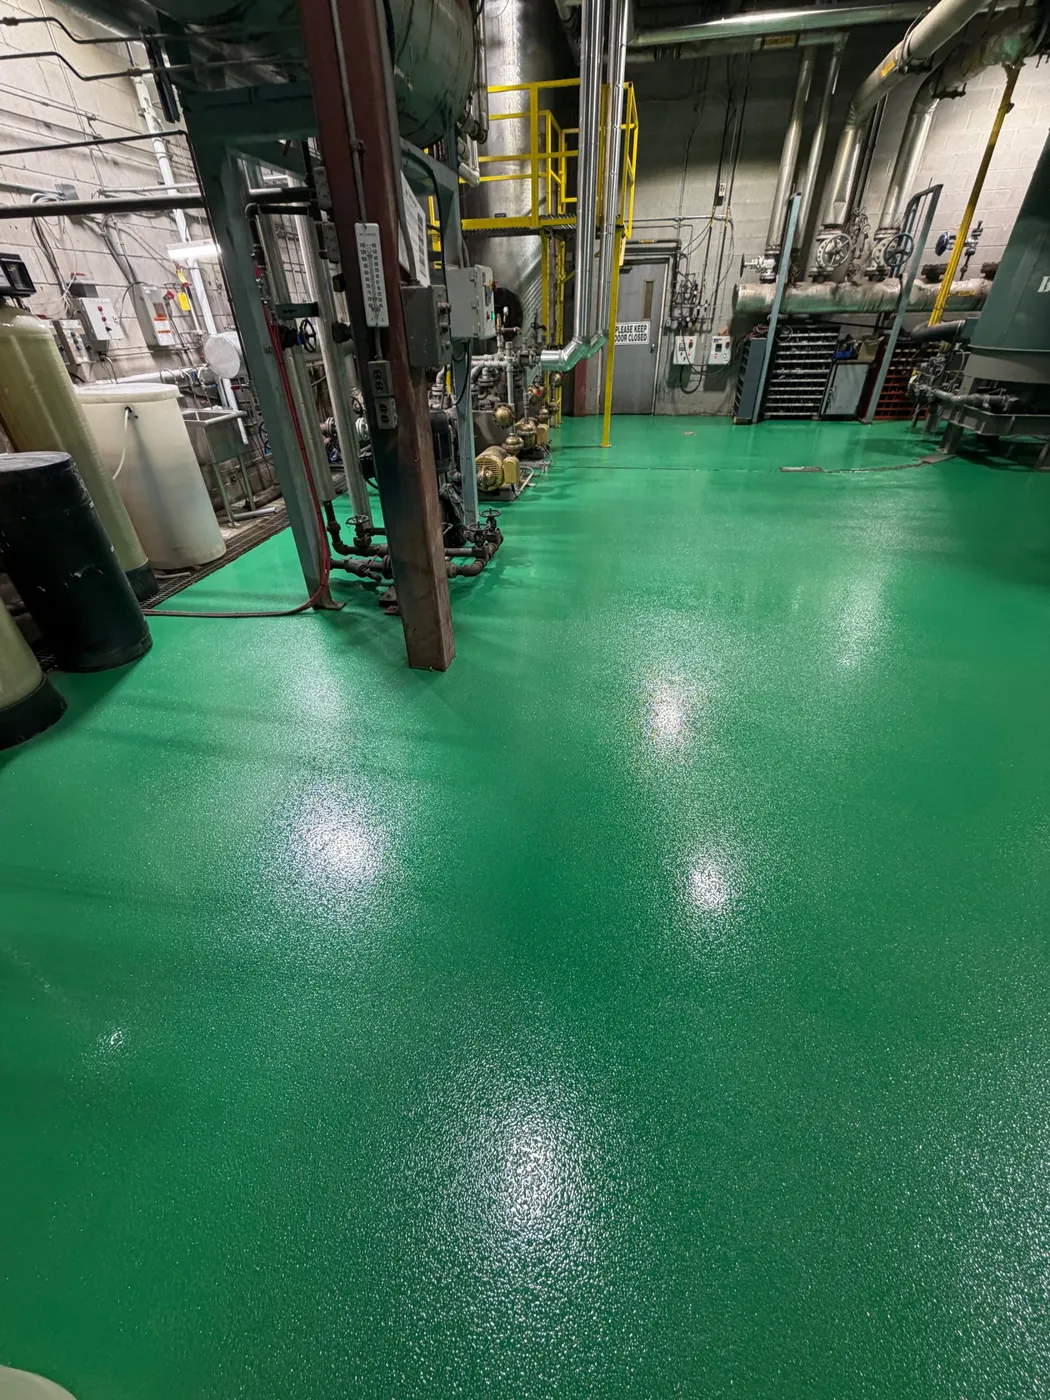
We installed a 2-coat solid colour Safety Green textured aggregate epoxy system. The concrete was prepared and coated around each piece of fixed equipment, and an aggregate was broadcast to give the finished floor a textured, slip-resistant surface. The Safety Green colour brightens the room and gives the plant a clean, consistent floor throughout the space.
Working Around Fixed Equipment
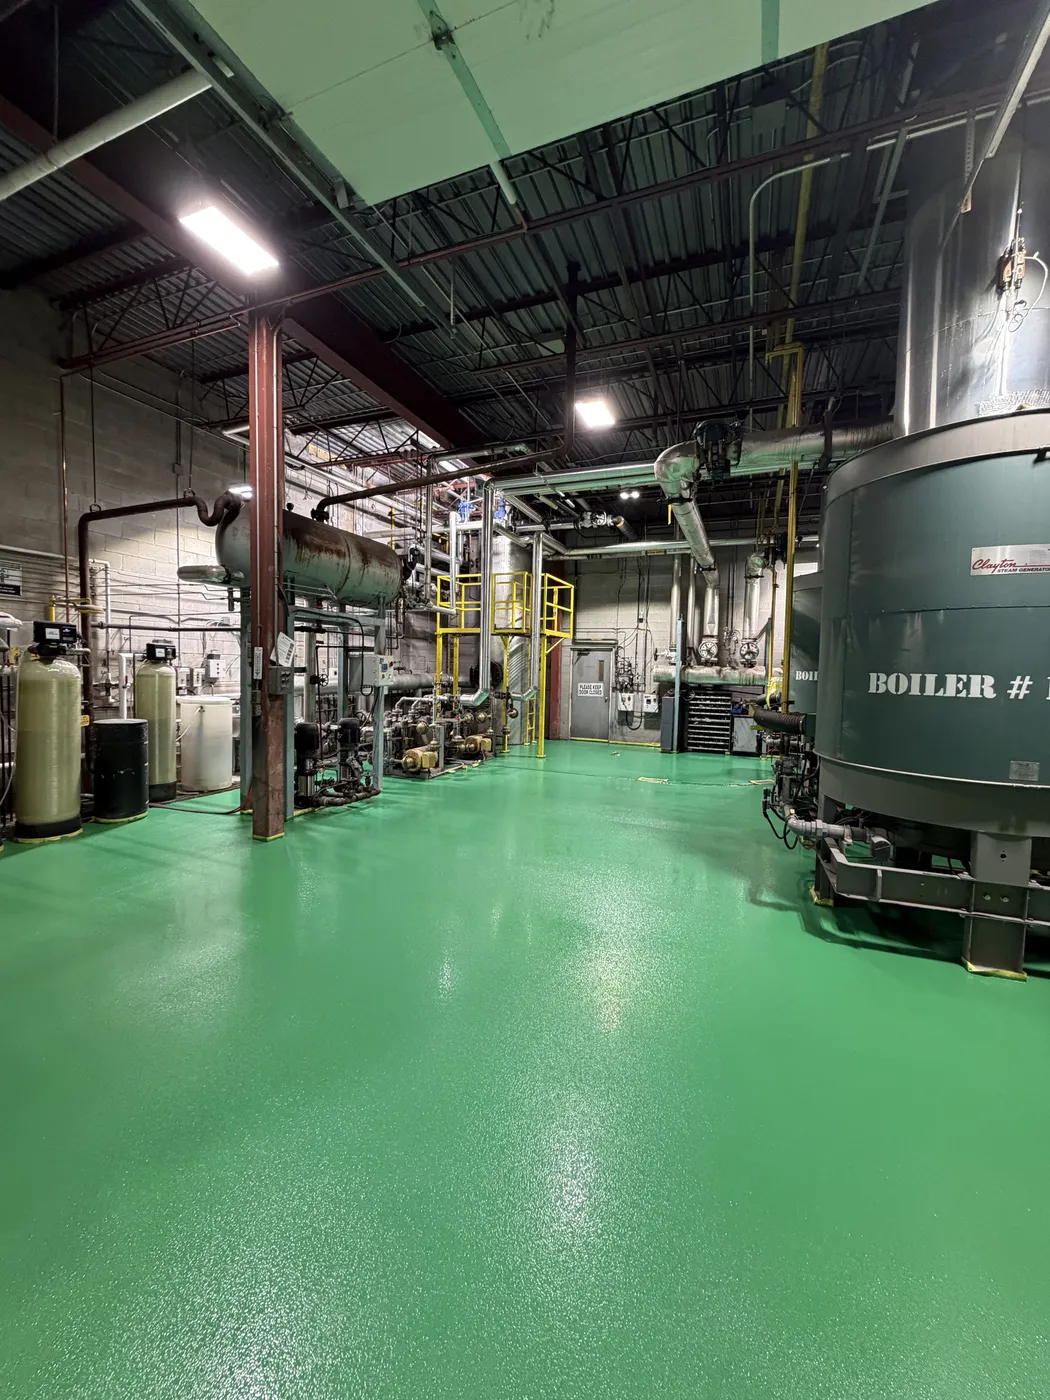
Boilers, pump skids, water treatment tanks and pipe supports stayed in place. The crew prepared and coated the floor around each base and support so the coating runs continuously through the room, with no bare concrete left between pieces of equipment.
The Result
- Approximately 2,000 sq ft of boiler room floor completed
- A 2-coat solid colour Safety Green epoxy system
- A textured aggregate finish for grip around pumps and piping
- A continuous, cleanable surface installed around fixed equipment
Floors for Food and Industrial Facilities
Production rooms, washdown areas, coolers and mechanical rooms each need a system matched to how the space is used. We review the slab, the equipment and your schedule, then recommend the system. See our food processing plant flooring and industrial epoxy flooring pages, or book a free site assessment.